← All products · Step 1 · Program
Posts Fusion programs straight to the MULTUS: probing, 5-axis, part transfer and bar pull, with no hand edits at the control.
▶ The 1-minute overview · captions, so it works with the sound off
Inspection Reporting
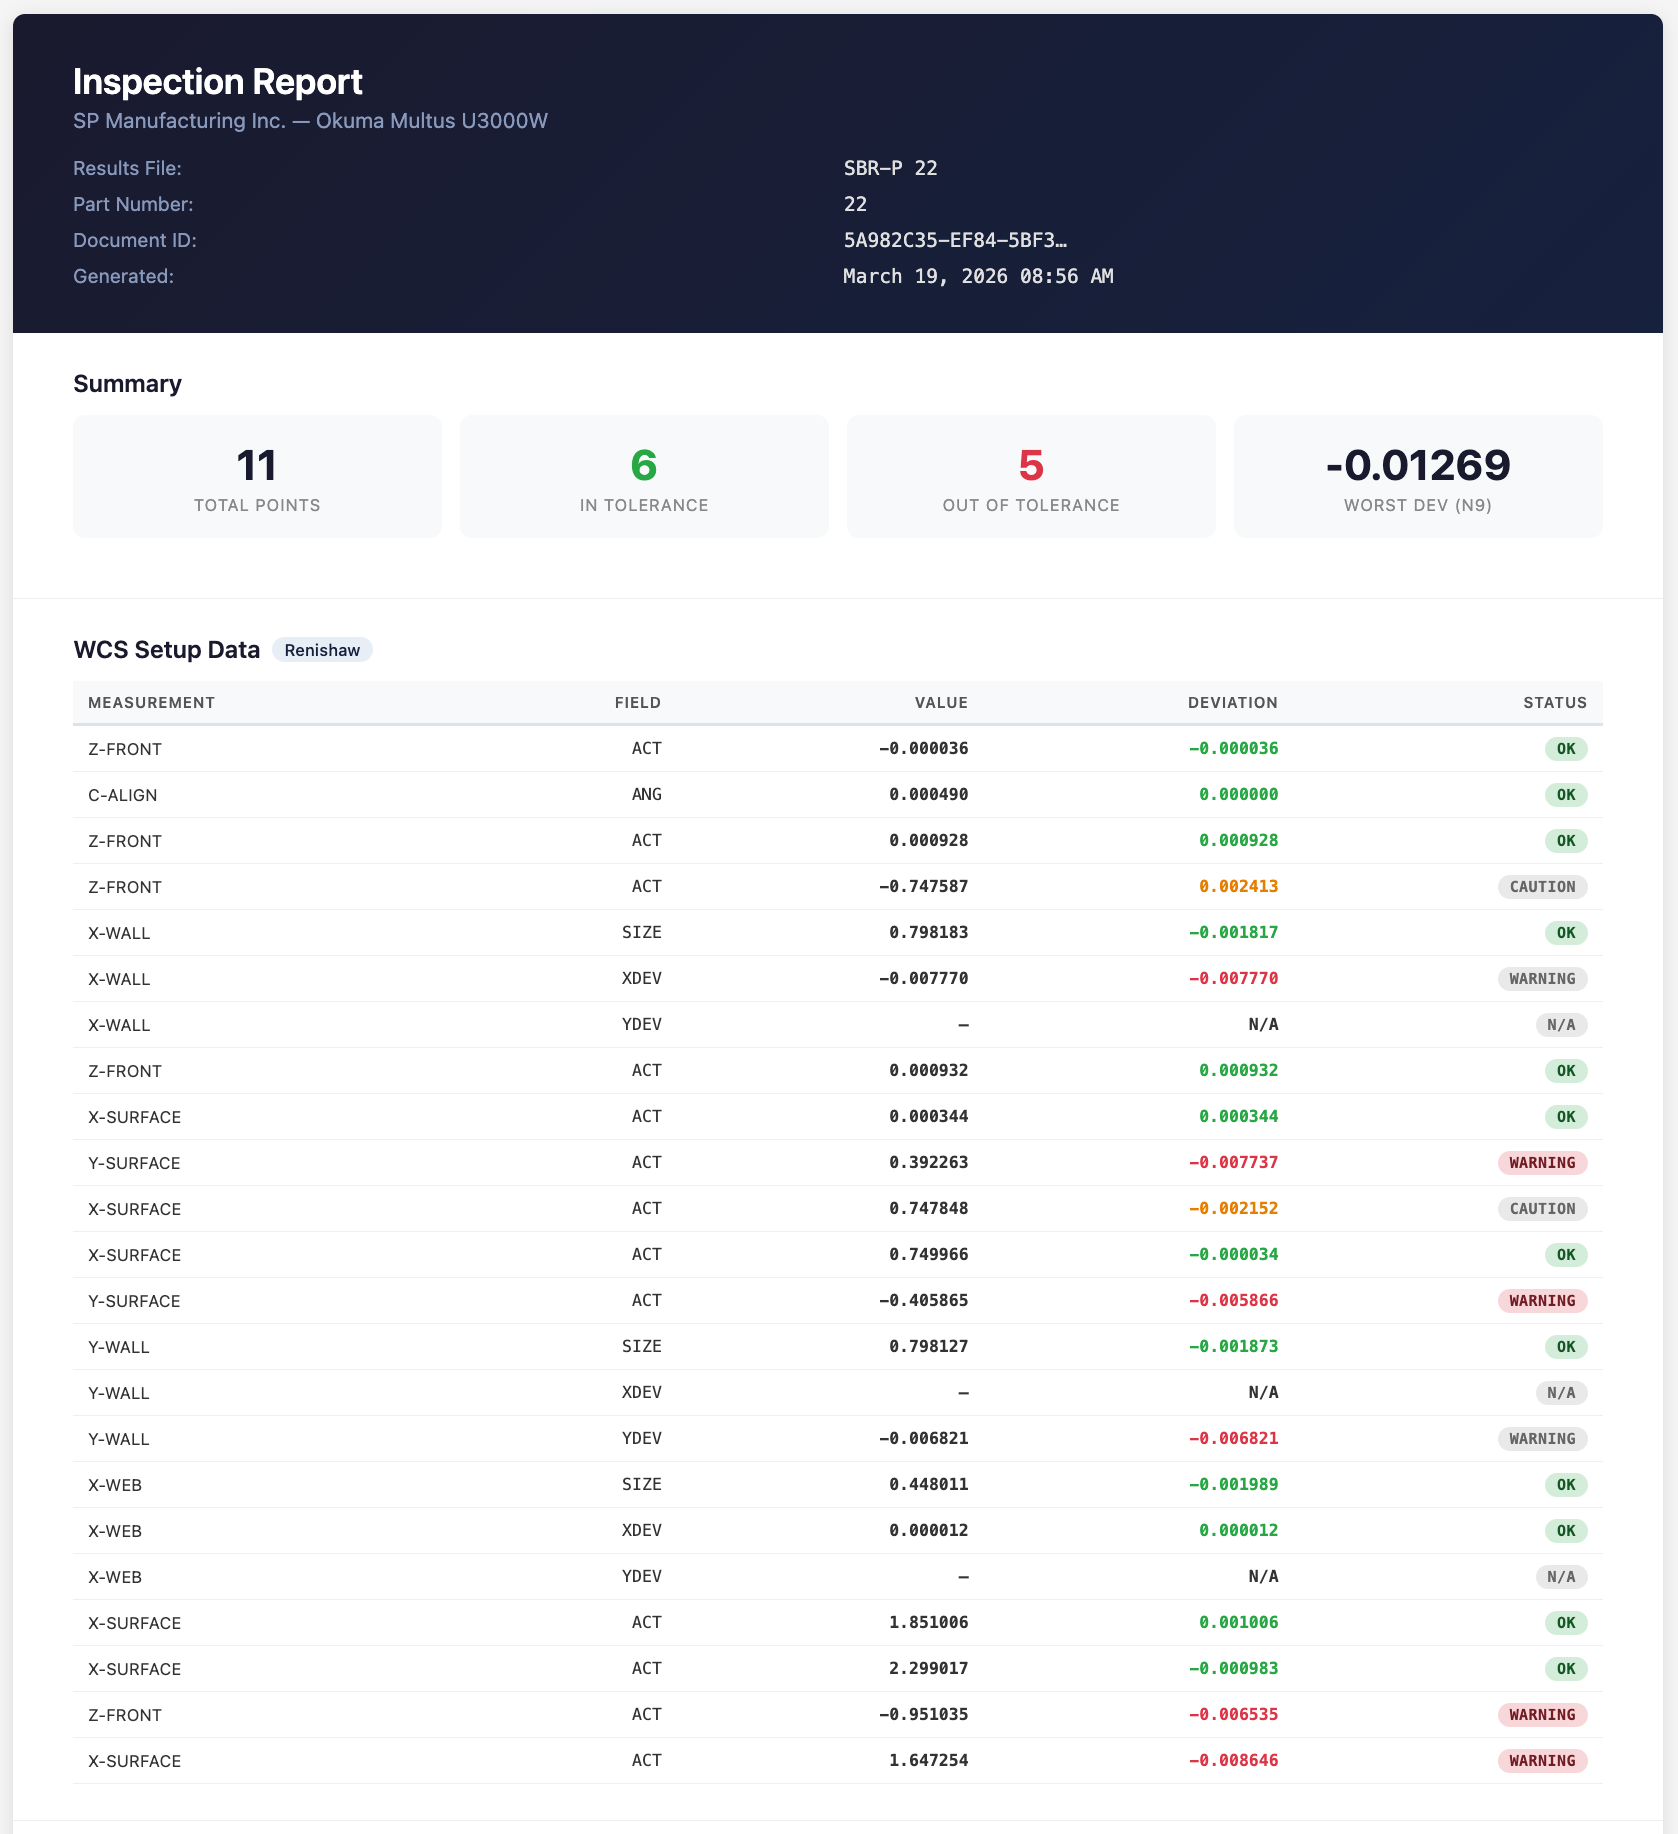
Renishaw probing cycles and Inspect Surface data flow straight from Autodesk Fusion to your Multus — no external software, no manual G-code. Every result lands on a single inspection report, mapped to part number and counting sequence.
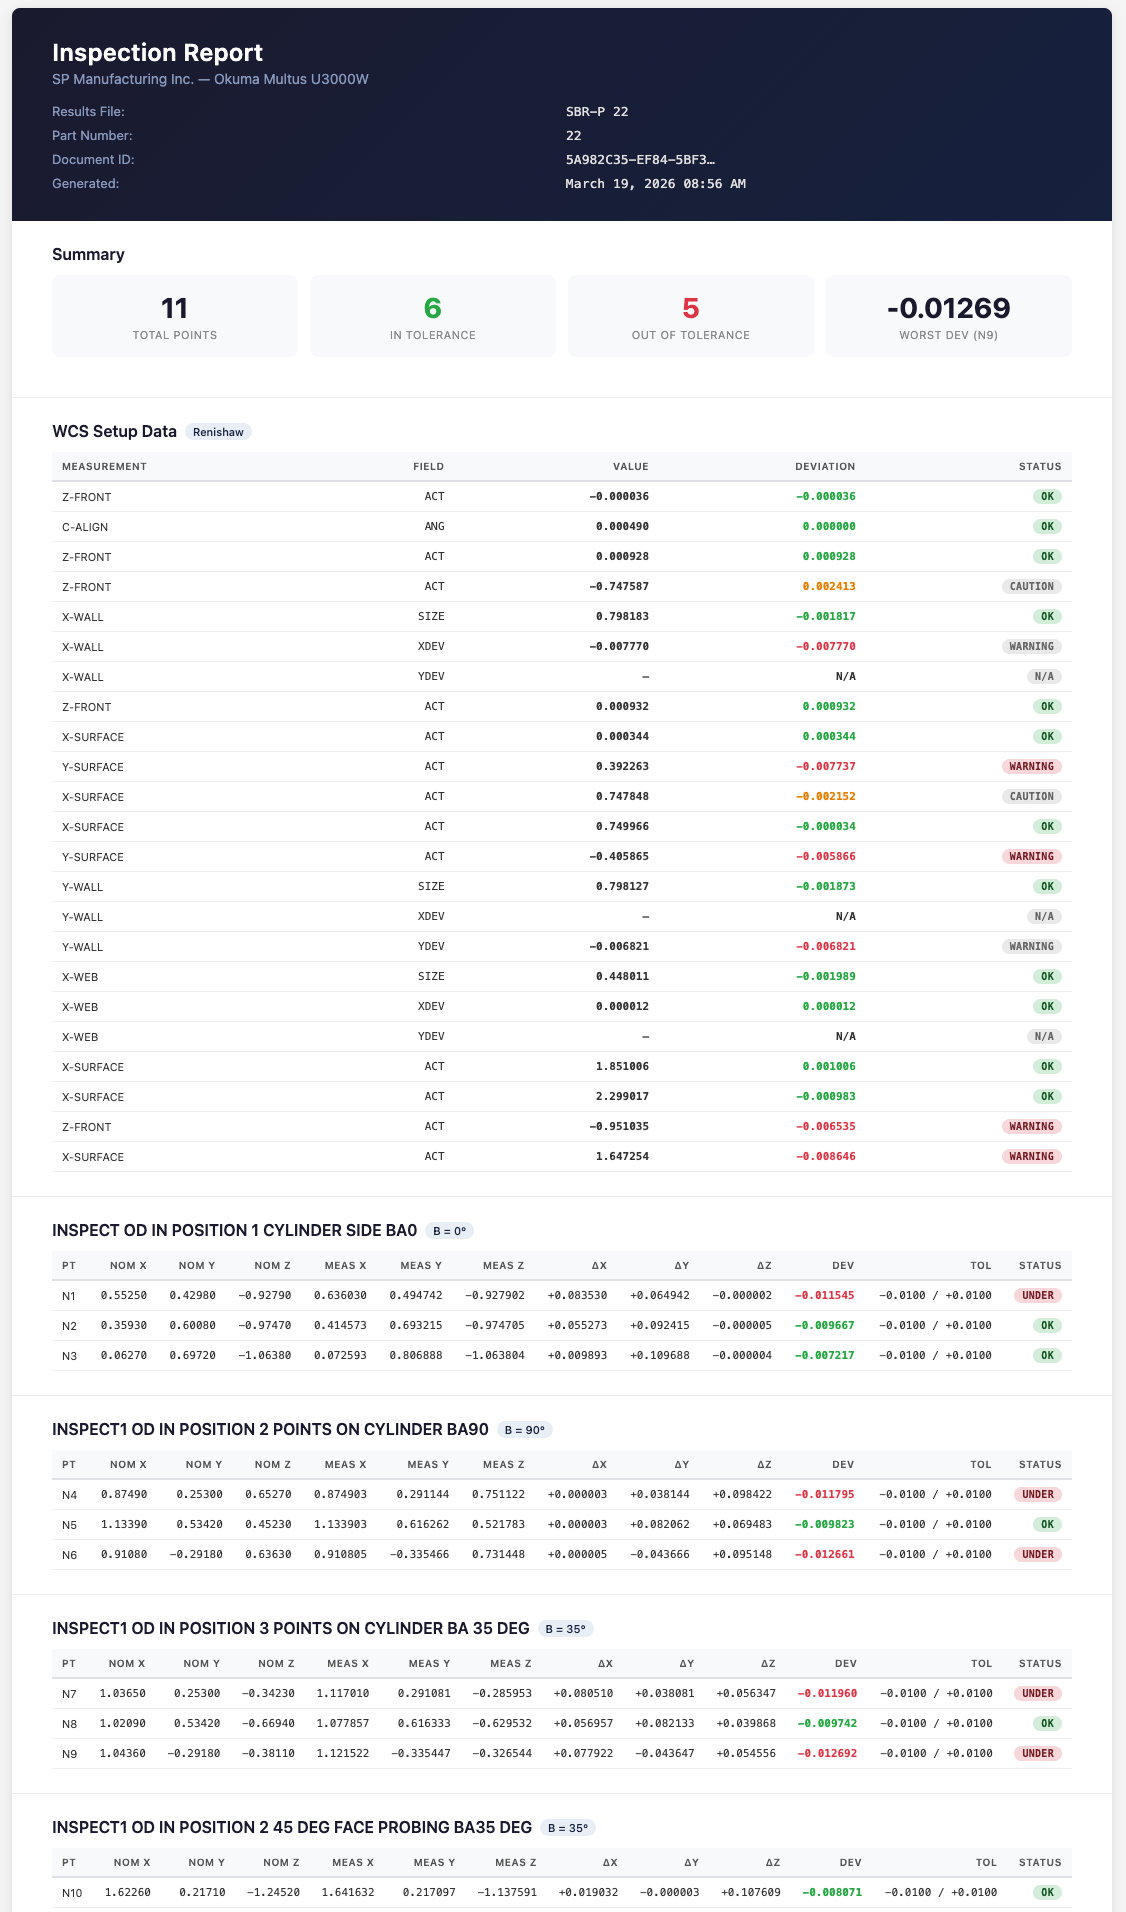
Every probing point reported with actual values, deviations, and pass/fail status — Z-front, X-wall, Y-surface, and more. Color-coded OK, warning, and caution at a glance.
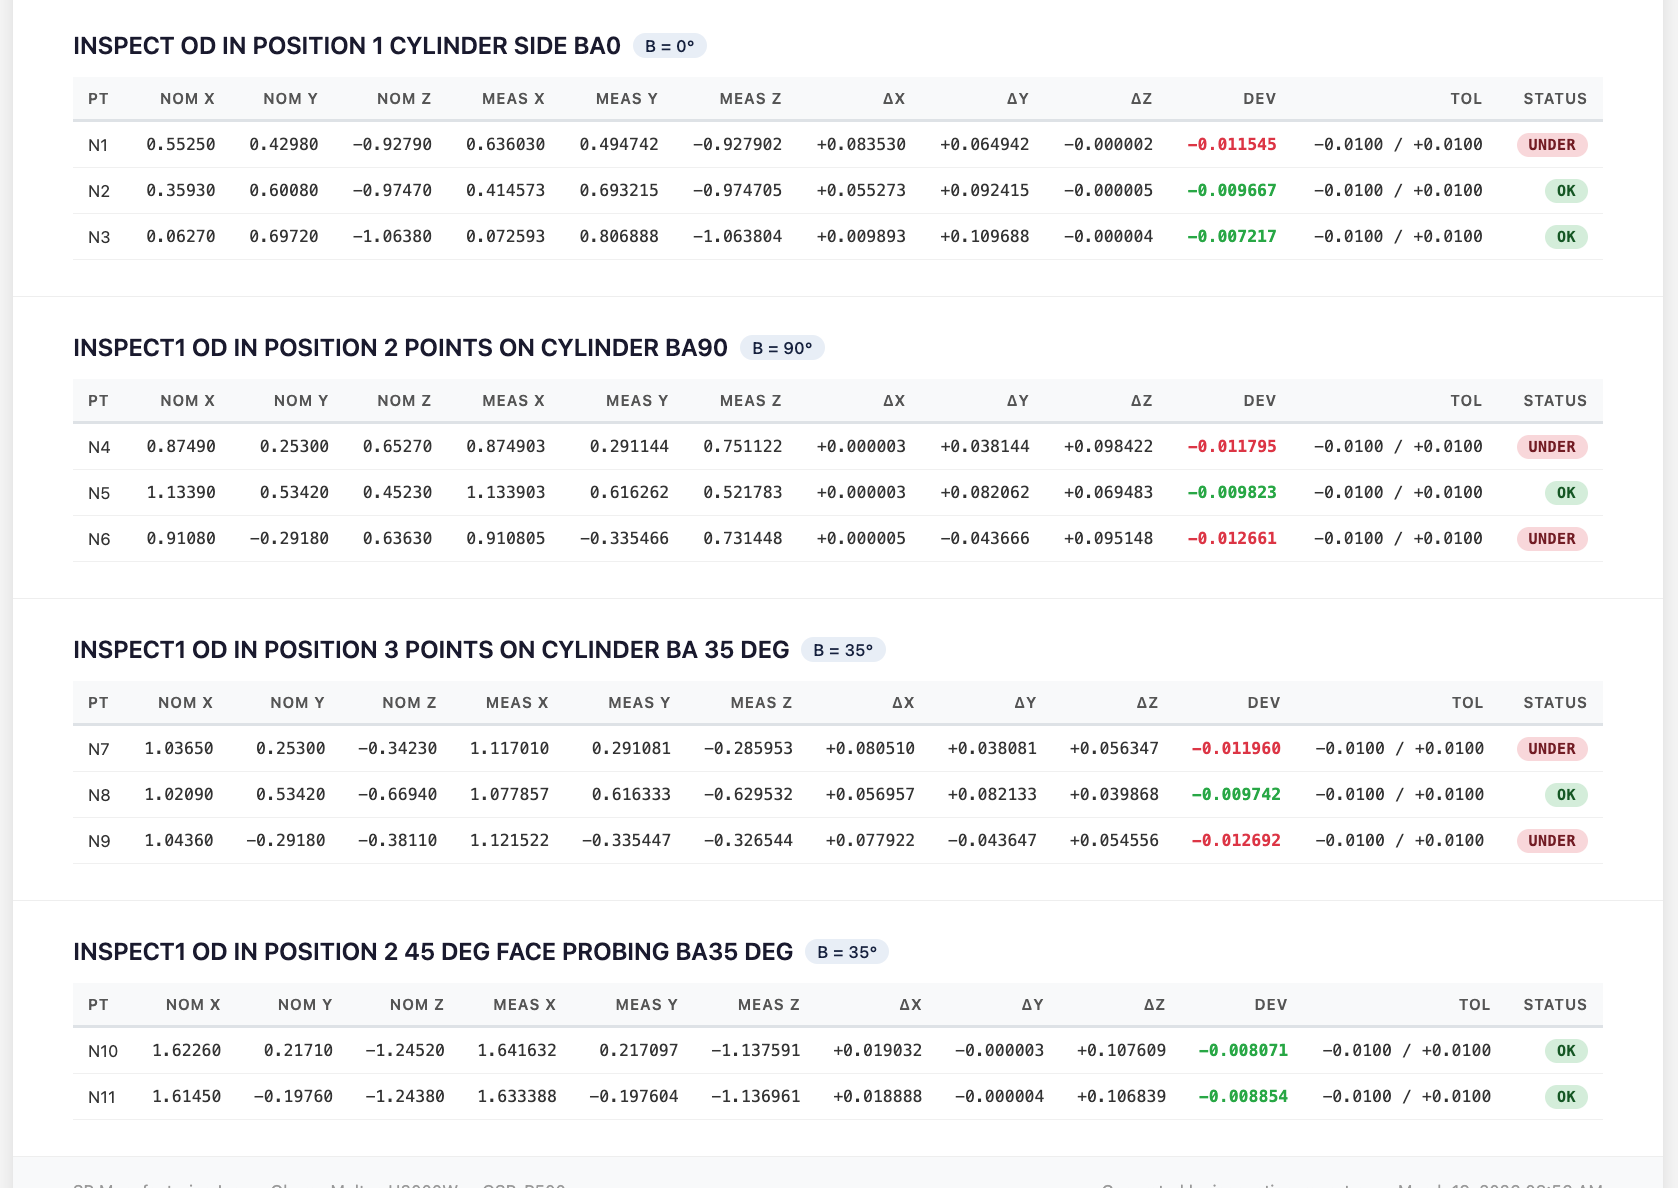
Fusion Inspect Surface output with OD measurements at multiple B-axis positions — cylinder probing at 0°, 90°, and 35° with nominal vs. actual comparison.
Everything on one report — Renishaw probing and surface inspection results together, tied to part number and counting sequence. One report, complete traceability.
See the Renishaw probing cycle simulated in Fusion 360 before posting the G-code to your Multus — verify every touch point before it hits the machine.
Probe to align the part and update work offsets, rough turn the OD, measure it, adjust cutter wear offset, recut to final dimension and verify — then the same closed-loop process for milling with cutter comp. All simulated in Fusion before posting G-code.
Import your probing results back into Fusion via the inspection post and see surface deviations projected directly onto the solid model. Instantly visualize where your part is in or out of tolerance — no separate software needed.
Renishaw probing and Fusion Inspect Surface measuring at different B-axis angles — verifying features from multiple orientations and renaming the output file with the correct part number.
The full closed loop, end to end: probe to set the work offset, machine the part, then Renishaw probing and Fusion Inspect Surface measure it in-process — measured results land back on the 3D model while the part is still clamped.
Post-to-Part Machining
Every video below was posted directly from Autodesk Fusion using our Advanced Post Processor — no hand editing, no patching. What you see in Fusion is what runs on the machine.
5-Axis Slot with Helical Start Bore
5-Axis Swarf Slot Groove with CAS
Bar Puller with SP Tooling Flange Mount
Large Part Machining with Fan
Long Part Machining Between Spindles
Deburr & Block Size Check
Post Processor Capabilities
One post processor covers the full range of Multus U-series operations. No manual G-code editing, no patching together multiple posts.
Full turning operations on both main and sub spindle with automatic spindle selection and handoff.
Simultaneous 5-axis milling on both main and sub spindle — positioned and continuous, live tooling included.
Automated part transfer between main and sub spindle — machine the front, transfer, and finish the back in one setup.
BK Mikro tool break detection integrated into the post — catch a broken tool before it damages your part or machine.
Full Renishaw inspection probing cycles posted directly from Fusion — measure features, log results, and generate reports.
Probe to establish and update work coordinate systems — align your part automatically before cutting.
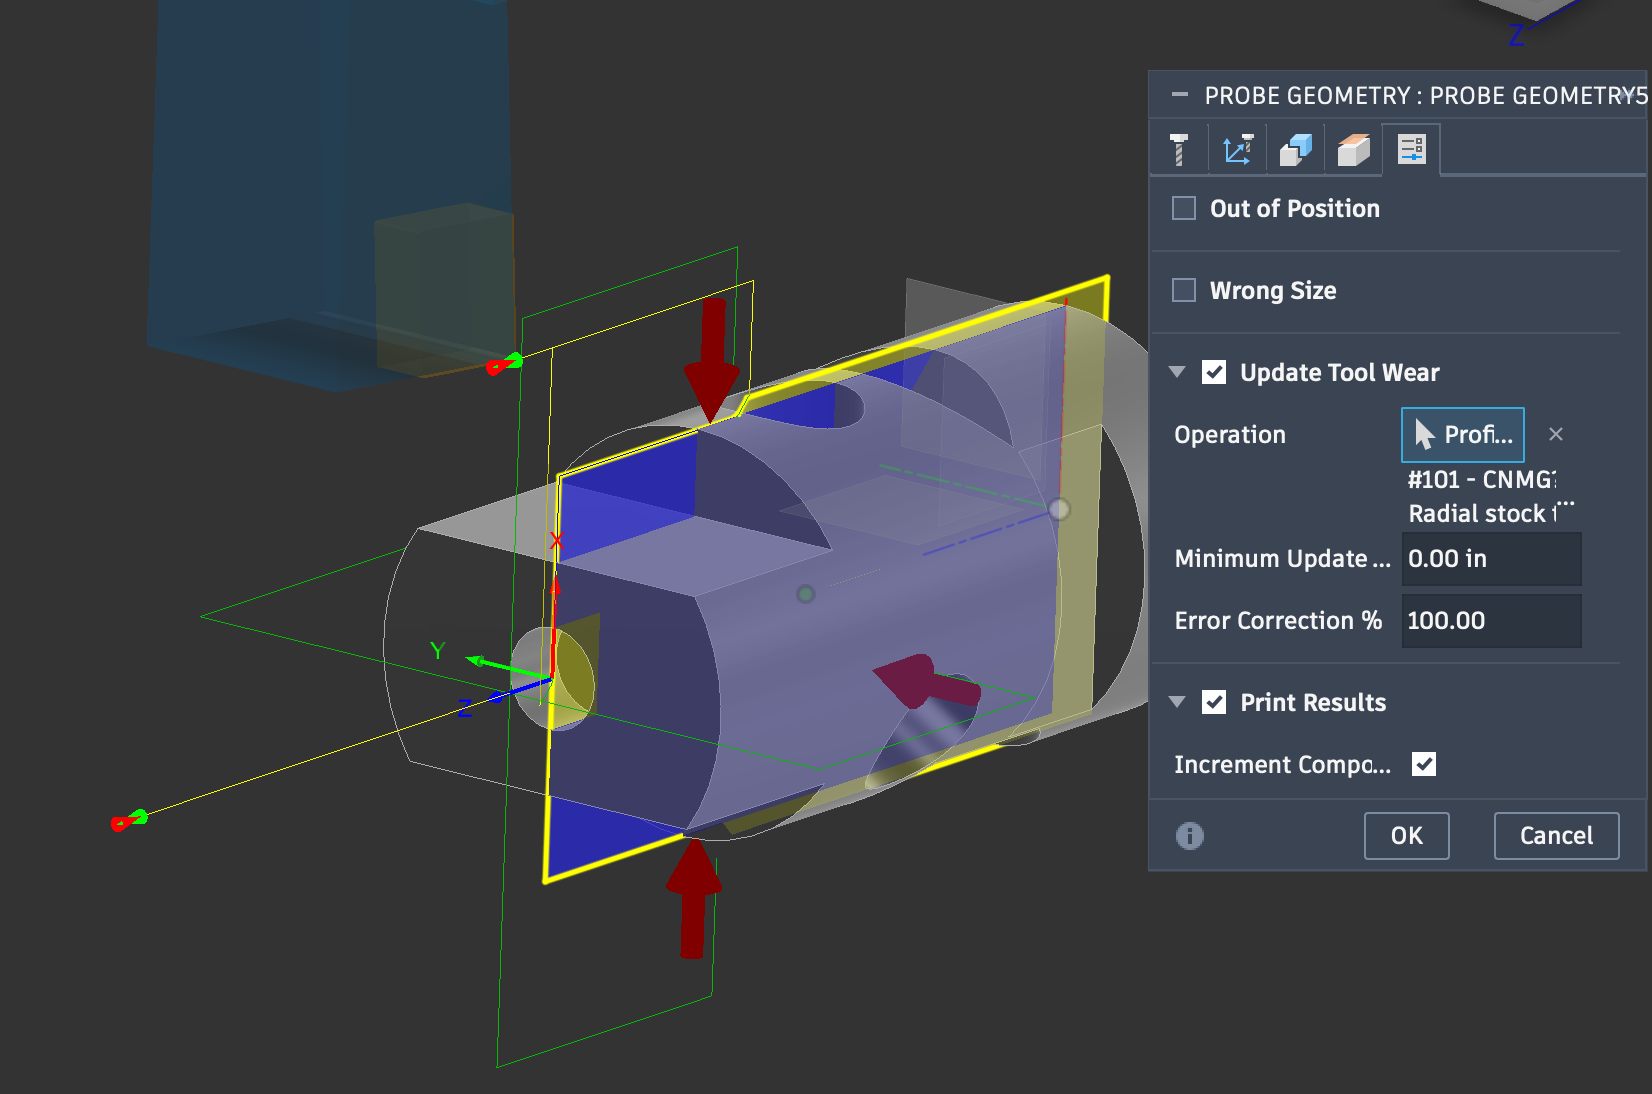
In-process measurement with automatic cutter wear offset adjustment — rough, measure, compensate, finish to final size.
Same closed-loop process for milling — probe, measure deviation, adjust cutter compensation, and recut to hit your tolerance.
Renishaw probe-based surface inspection posted from Fusion — results imported back and projected onto the 3D model for visual deviation analysis.
Developed in conjunction with Gosiger AE, M360 is a custom macro that fully resets and recovers the Multus U-series with a 95% success rate — no operator input required.
Resetting a multitask machine is time-intensive and requires deep knowledge — homing Y and X axes, resetting B axis, restaging tools, and more. M360 handles it all automatically, and the post processor calls it to get the machine back to cutting parts as fast as possible. Exception: tool magazine issues cannot be handled yet, as this is a PLC-level problem.
How It Works
Two diagrams that show exactly how our post processor fits into the Fusion 360 → CNC workflow, and how the closed-loop cutter compensation and wear adjustment process works automatically.
Okuma Multus Series · OSP-P500 · SP-Tooling-Apps
Advanced Probing Workflow · Okuma Multus Series · SP-Tooling-Apps
Fusion 360 Probe Geometry — Update Tool Wear with 3D part model and probing vectors
Get in touch for pricing, a demo, or to talk shop. Built by machinists — happy to talk machinist.
Thanks, we have your request. We will email you to set up a time.